
 Oct 27,2026
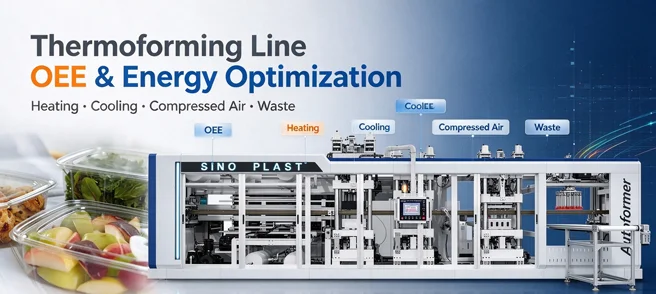
A plastic thermoforming line can run without breakdowns and still lose money through slow cycles, hidden energy waste, and scrap that never gets measured. The two numbers that expose this gap are OEE and energy cost per good part. This playbook explains how to measure both, where energy actually goes on a thermoforming line, and how to improve the five levers that matter most: heating, cooling, compressed air, scrap, and mold change. It closes with a 30-day framework and a practical note on data monitoring.
OEE is not a maintenance metric. It is a production metric that tells you how much of the planned production time is converted into good parts. In a thermoforming context, it exposes three distinct loss types that require different interventions.
A line at 85% availability, 80% performance, and 95% quality has an OEE of approximately 65%. That means roughly one-third of planned production time is lost to some combination of stops, speed loss, and defects.
The diagnostic value is in separating the three. A line with high availability but low performance needs a different intervention than a line with high performance but frequent breakdowns. Without measurement, improvement is guesswork.
A practical OEE template does not need to be complex. The following fields are enough to start:
| Field | Definition | Example Entry |
|---|---|---|
| Shift length | Total scheduled time | 480 min |
| Planned downtime | Breaks, planned maintenance | 30 min |
| Planned production time | Shift length − planned downtime | 450 min |
| Unplanned downtime | Breakdowns, material waits, quality holds | 40 min |
| Actual production time | Planned production time − unplanned downtime | 410 min |
| Availability | Actual production time ÷ planned production time | 410 ÷ 450 = 91.1% |
| Ideal cycle time | Rated seconds per cycle | 2.0 s |
| Total parts produced | Count of all parts | 8,000 |
| Theoretical output | Actual production time ÷ ideal cycle time | 410 × 60 ÷ 2.0 = 12,300 |
| Performance | Total parts produced ÷ theoretical output | 8,000 ÷ 12,300 = 65.0% |
| Good parts | Parts meeting quality standard | 7,600 |
| Quality | Good parts ÷ total parts produced | 7,600 ÷ 8,000 = 95.0% |
| OEE | Availability × Performance × Quality | 91.1% × 65.0% × 95.0% = 56.3% |
The example shows a line with strong availability and good quality but weak performance. The improvement priority is performance—cycle time, cooling, material consistency, or operator behavior—not breakdown reduction.
Start with manual shift logs: downtime reason, cycle count, reject count. More advanced setups pull machine states from the PLC via OPC UA or similar protocols and calculate OEE in real time. The template above is also the basis for the downloadable OEE calculation sheet referenced at the end of this guide.
Before optimizing energy, know where it goes. The split depends on machine type and whether sheet extrusion is inline.
For plate thermoforming machines, heating accounts for more than 70% of energy demand; the rest is motors, compressed air generation, and cooling. For roll-fed automatic machines and inline extrusion-thermoforming setups, the picture shifts: compressed air and heating the semi-finished sheet can together account for up to 60% of the thermoformer’s total energy requirement.
At the cup manufacturing level, industry references indicate energy costs of roughly 15–25% of total production cost, with electricity consumption in the range of 0.8–1.5 kWh per thousand cups, depending on machine efficiency and production parameters. A typical thermoforming machine draws approximately 15–45 kW during active production.
| Machine / Line Type | Dominant Energy Load | Planning Implication |
|---|---|---|
| Plate thermoforming | Heating (>70%) | Focus on radiation efficiency, zoning, insulation |
| Roll-fed automatic | Compressed air + heating (up to 60% combined) | Audit leaks, optimize vacuum, check heater control |
| Inline extrusion + thermoforming | Heating + extruder drive + cooling | Coordinate sheet residual heat, extruder efficiency, chiller load |
| Cup line (summary metric) | 0.8–1.5 kWh per 1,000 cups | Track per-1,000-part energy as a KPI |
These are planning references, not guarantees. Actual consumption varies by material, thickness, cycle time, mold design, and ambient conditions.
PET and PP behave differently in the heating and forming stages, and that difference affects energy demand.
| Factor | PET | PP |
|---|---|---|
| Typical sheet heating range | Lower temperature window, but sensitive to moisture | Higher temperature window, broader processing range |
| Drying requirement | Usually requires drying before forming | Less moisture-sensitive than PET |
| Cycle speed potential | Often faster at equal thickness in well-controlled conditions | Generally slower than PET at equal thickness |
| Cooling sensitivity | Moderate | Higher; thicker sections and crystalline behavior affect cooling |
| Energy implication | Drying adds energy load; forming energy may be lower per cycle | Heating energy may be higher per cycle; cooling load can be significant |
The practical benchmark is not a single number but a trend: for the same product family, compare kWh per 1,000 good parts between PET and PP runs on the same line. If the gap is larger than expected, check drying, heating zones, and cooling setpoints before assuming the material is the cause.
Total plant electricity bills cannot separate heating, compressed air, and cooling. Sub-metering makes the split visible.
A practical sub-metering scope:
Even a temporary clamp-on power logger on the main supply and the heating circuit for one week provides a usable baseline. Permanent sub-metering is justified when the line runs continuously and energy cost is a significant share of production cost.
For lines where energy data collection or remote support is part of the equipment specification, confirm the available interfaces and protocols during the purchasing process. The plastic thermoforming machine page lists available configurations; the Sinoplast team can confirm what data outputs are available for a specific model.
Heating is the largest single energy load on most thermoforming lines. Improvements come from three areas: radiation source, control strategy, and thermal environment.
Ceramic infrared radiators with integrated thermal insulation have shown measurable savings versus conventional full-ceramic designs. In controlled evaporation tests representative of thermoforming heating tasks, ELSTEIN HTS-series radiators required about 0.193 kWh versus 0.229 kWh for a conventional FSR radiator and 0.277 kWh for another manufacturer’s FSR design—roughly 15% lower than the first comparator and about 30% lower than the second. The savings potential improves when the heating task has a shorter cycle time. Other infrared systems have reported reductions of 40% or more versus older Calrod heaters in measured tests.
Zoning lets different sheet areas receive different energy inputs, which matters for uneven wall thickness or complex geometry. PID control holds zone temperature more stably than on/off control, reducing overshoot and unnecessary energy input. Integrated insulation on the radiator back reduces heat loss to the frame and surrounding air. Enclosing the heating station or adding heat shields further reduces losses.
The goal is not maximum heater power. It is the minimum energy that still produces consistent forming.
The heating curve—how sheet temperature rises over time in the oven—affects both quality and energy use.
For each material, the practical method is the same: start from the material supplier’s recommended sheet temperature range, verify actual sheet temperature at the oven exit, and adjust zone setpoints and line speed together. Changing only one variable usually moves the problem rather than solving it.
Three actions usually produce the first measurable reduction without touching product quality:
Measure energy per 1,000 parts before and after any heater or control change. Without that number, improvement is assumed rather than verified. For a broader view of how the sheet extrusion stage affects downstream forming energy, see the article on what benefits a high-speed PP/PS sheet extruder brings.
Thermoforming uses positive and negative pressure to form sheet into the mold. Compressed air and vacuum are core utilities—and common waste sources. Industry experience suggests that nearly half the air produced in a typical plastics plant may be wasted through leaks, improper use, and artificial demand. This is not thermoforming-specific, but it indicates the scale.
A leak audit is low-cost and usually produces actionable findings within days.
Cooling affects both quality and cycle time. If the mold runs too hot, cycle time must extend; if cooling is uneven, warping and dimensional variation increase.
Cycle time is often limited by how fast the part can be cooled to a stable shape. If cooling is insufficient, the part may deform after ejection, causing dimensional variation and scrap. Uneven cooling—hot spots on one side of the mold—produces warping even when average mold temperature looks correct.
The practical diagnostic sequence:
Cooling inefficiency often shows up as slower cycles and higher scrap—both OEE losses. For problems that appear as warping, short shots, or surface defects, the common thermoforming problems and solutions guide covers the diagnostic path in more detail.
Scrap is both a Quality loss and a material cost. Levers fall into three categories.
| Lever Category | Examples | Typical Action |
|---|---|---|
| Material | Sheet thickness tolerance, moisture content, regrind quality | Verify incoming sheet and drying conditions |
| Mold | Cutting edge condition, vacuum holes, surface quality | Inspect and maintain tooling on a cycle-based schedule |
| Process | Heating uniformity, forming pressure/vacuum, cooling time, plug assist | Tune parameters against a measured process window |
Many scrap problems attributed to “bad material” are actually process window issues. A scrap Pareto by product, shift, and defect type usually shows that a small number of causes account for most of the loss. For a focused list of scrap-reduction actions, see 5 ways to minimize scrap rate on your plastic thermoforming machine.
Changeover time is an Availability loss. In thermoforming, mold changes involve stopping production, removing the old mold, installing and aligning the new mold, connecting cooling and vacuum, setting parameters, and running trial parts until quality is acceptable.
SMED (Single-Minute Exchange of Die) separates internal setup (machine stopped) from external setup (machine running).
Published case studies on thermoforming lines have reported setup time reduced from 56.25 minutes to 22.3 minutes—more than 60%—contributing to availability improvement from 80% to 93% when combined with TPM and standardized work. Another study reported changeover reduced to around 8 minutes after redesigning mold mounting elements.
Practical SMED actions:
The biggest gains usually come from externalizing work, not from making the technician faster. If the mold is already at the machine, the tools are laid out, and the parameters are pre-loaded, the internal setup time drops even without new equipment.
A simple setup checklist:
Specific savings depend on machine and mold design. For lines where changeover frequency is high, the article on frequent mold changeover downtime discusses the upgrade path in more detail.
OEE and energy improvement become durable when they are measured continuously rather than reconstructed from memory at month-end.
| Level | What It Looks Like | What It Enables |
|---|---|---|
| Manual | Shift logs for downtime, output, rejects; monthly energy bills | Baseline OEE and energy per 1,000 parts |
| Semi-automatic | PLC counters, reason codes, sub-metered energy for heating/air/cooling | Faster diagnosis of loss categories |
| Dashboard | OEE and energy KPIs visible to shift teams; alarm logs | Daily management and accountability |
| Connected | Remote diagnostics, predictive alerts on heaters, drives, vacuum | Faster service response and condition-based maintenance |
Alarm management matters more than dashboard aesthetics. An alarm that fires ten times a shift and is ignored trains operators to ignore all alarms. Start with a small set of alarms tied to OEE losses—unplanned stop, low vacuum, heater deviation, chiller alarm—and review them daily.
Remote diagnostics allow the machine builder to review PLC data and alarm history without traveling to site. This can shorten troubleshooting time and reduce MTTR, especially for electrical and control issues.
Predictive maintenance uses sensor data—vibration, temperature, pressure, cycle time—to detect degradation before failure. It is useful when a baseline of reliable maintenance data exists, and the organization has routines to act on alerts. A plant without autonomous and planned maintenance will struggle to use predictive data effectively, because there are no routines to respond to the alerts.
For equipment models featuring data collection and remote support as standard specifications, please verify supported interfaces and communication protocols at the time of purchase. Our Sinoplast machine quality page details our manufacturing standards and equipment inspection procedures, while the Sinoplast Service page outlines installation, operator training, and after‑sales support packages.
This is a starting structure, not a guaranteed result. Actual savings depend on baseline conditions, material, and operating discipline.
Week 1 — Measure the baseline.
Week 2 — Find the largest losses.
Week 3 — Implement no-cost and low-cost actions.
Week 4 — Re-measure and standardize.
Savings ranges depend heavily on the baseline. The following are planning references from published sources, not guarantees for a specific line:
| Improvement Area | Reported Range | Source Context |
|---|---|---|
| Insulated ceramic infrared radiators vs conventional designs | ~15–30% lower heating energy in controlled tests | Laboratory evaporation tests, not production lines |
| Infrared vs older Calrod heaters | 40% or more reduction in measured tests | Equipment comparison tests |
| Compressed air waste | Up to ~50% of air produced may be wasted in typical plastics plants | Cross-industry observation, not line-specific |
| SMED changeover reduction | 50–60% reduction reported in published thermoforming case studies | Specific case conditions |
For payback estimation, use the plant’s own baseline: energy cost per 1,000 parts before the change, the measured reduction after the change, and the investment cost (equipment, installation, downtime). A simple formula:
Payback (months) = Investment cost ÷ Monthly savings
If sub-metering is not available, use a conservative estimate and verify with a temporary power logger before committing to a larger investment.
OEE = Availability × Performance × Quality. Availability is actual production time divided by planned production time. Performance is actual output divided by theoretical output at rated cycle speed. Quality is good parts divided by total parts produced. Record downtime reasons, cycle counts, and reject counts per shift to calculate all three factors.
Industry references indicate energy costs of roughly 15–25% of total production cost for cup manufacturing, with electricity consumption around 0.8–1.5 kWh per thousand cups and machine draw of approximately 15–45 kW during active production, depending on machine size and configuration. These are planning ranges; measure the specific line for actual figures.
Start with heating, which is the largest load on most lines. Verify zone setpoints against actual sheet temperature, check insulation and heat shields, and match line speed to heating capacity. Then audit compressed air leaks and cooling setpoints. Measure energy per 1,000 good parts before and after each change so that savings are verified rather than assumed.
Use an ultrasonic leak detector during production and check fittings, solenoid valves, hoses, and cylinder seals. Also verify mold vacuum holes are clear and vacuum lines are not leaking. Log each leak with location and estimated flow, repair in priority order, and re-check after one month. Industry experience suggests a significant share of compressed air in plastics plants is wasted, so audits often find quick wins.
Insufficient or unstable cooling causes warping, dimensional variation, and surface defects. If the chiller cannot hold the setpoint, cycle time must extend to compensate, reducing performance. Uneven flow across mold circuits creates hot spots that produce warping even when average mold temperature looks correct. Check chiller capacity, flow balance, and mold channel condition before adjusting process parameters.
Work through three categories: material (sheet thickness tolerance, moisture, regrind ratio), mold (cutting edge, vacuum holes, surface condition), and process (heating uniformity, forming pressure, cooling time, plug assist). Build a scrap Pareto by product, shift, and defect type to find the largest cause, then address that cause first. For food-contact products, confirm regrind use against the applicable regulatory framework.
OEE and energy cost are connected. A line that runs slowly to compensate for cooling problems, leaks compressed air through worn fittings, or scraps parts because heater zones are not controlled is losing money on both dimensions at once. Start with measurement: availability, performance, and quality for OEE; kWh per 1,000 good parts for energy. Then let the largest loss category point to the first action.
For lines where cycle time, heating configuration, or auxiliary equipment sizing is the limiting factor, review the machine and auxiliary specifications against actual production requirements. The plastic thermoforming machine and plastic cup making machine pages show available configurations. To discuss a specific line’s OEE or energy baseline, contact the Sinoplast team through Contact Us.
Download the OEE calculation template used in this guide to record availability, performance, quality, and energy per 1,000 parts for your own line. For a focused review of your line’s energy and OEE baseline, request an energy audit with the Sinoplast engineering team, or reach the team directly on WhatsApp for a quick technical discussion.
Oct 27,2026
We are a professional plastic machinery provider in China.